
Define the limited adjustment function
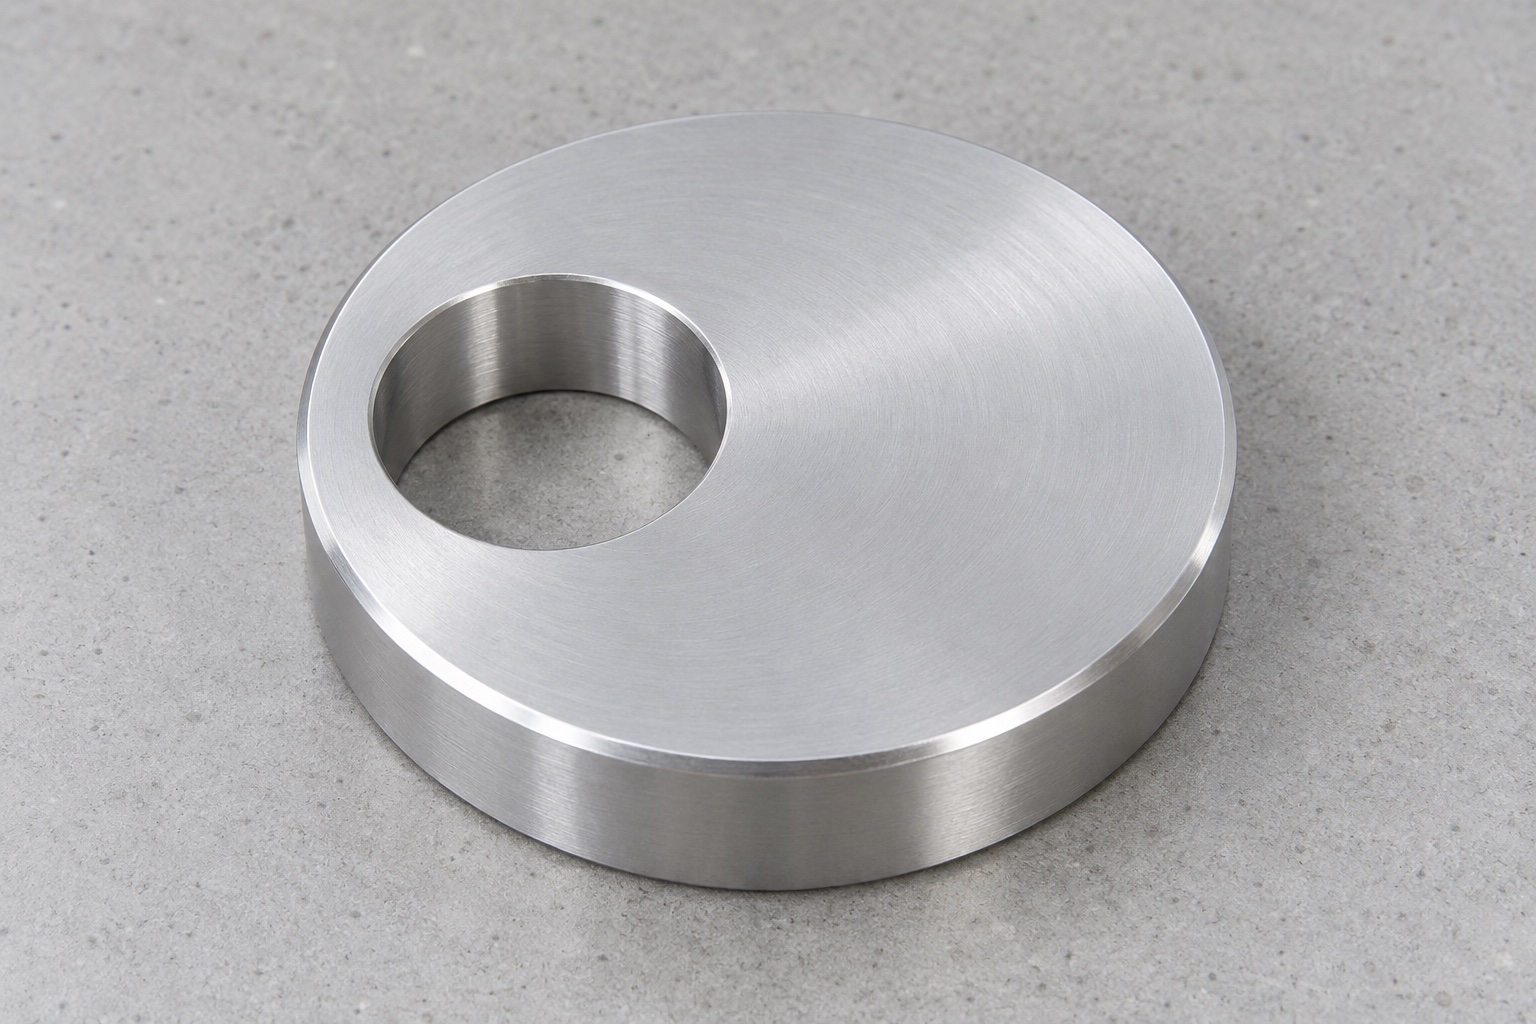
An equipment-side service mechanism in a medical laboratory instrument may use an eccentric disc to change a mechanical contact position before a separate arrangement holds the setting. The illustrative part is a thick flat circular aluminum disc with one plain off-center through hole, opposite flat faces and no thread or additional feature. No actual assembly or manufactured specimen is shown. The disc is not an independently locked adjuster, a calibrated scale or a qualified medical positioning system. The designer must define the moving contact, support, permitted rotation and holding method before the supplier can establish a manufacturing scope.

Identify the two intended axes
Obtain the controlled disc drawing and model, actual mounting member, mating contact and device revision. Distinguish the circular exterior's geometric axis from the bore axis. Specify their approved offset and the references used to establish it. A hole diameter and outside diameter alone do not define the eccentric relationship. A bore that looks visibly displaced in an image supplies neither an approved offset nor a measured result. Clarify the intended mounting and contact arrangement instead of centering the opening for convenience or accepting a familiar washer-like outline as a complete mechanical drawing.
Relate rotation to the actual contact arrangement
The useful change in contact position depends on the disc's installed orientation, the mating surface and the permitted range of movement. Do not convert an apparent offset directly into a universal travel, resolution or force claim. Review the full rotation envelope and possible interference with supports, cables, fasteners and nearby mechanisms. The equipment documents should identify allowable settings and access for adjustment. A disc that can rotate freely on a bench may not offer the intended useful motion after assembly. Any travel limits, setting marks or tool features require explicit controlled definition rather than assumptions from the illustration.
Define the bore as a real mounting interface
Specify bore size, through depth, entry treatment and required relationships to useful faces. Identify whether the actual connection uses clearance or another approved fit, and define the separate mounting and retaining components. A simple cylindrical hole does not by itself prevent axial removal or preserve an angular setting. Do not add a keyway, thread, cross hole or hidden fastener to complete an ambiguous design. Resolve missing requirements with the responsible equipment team. A convenient rod passing through one sample is not a substitute for the bore specification or evidence that the installed adjustment can be held during service.
Control the exterior and face contacts
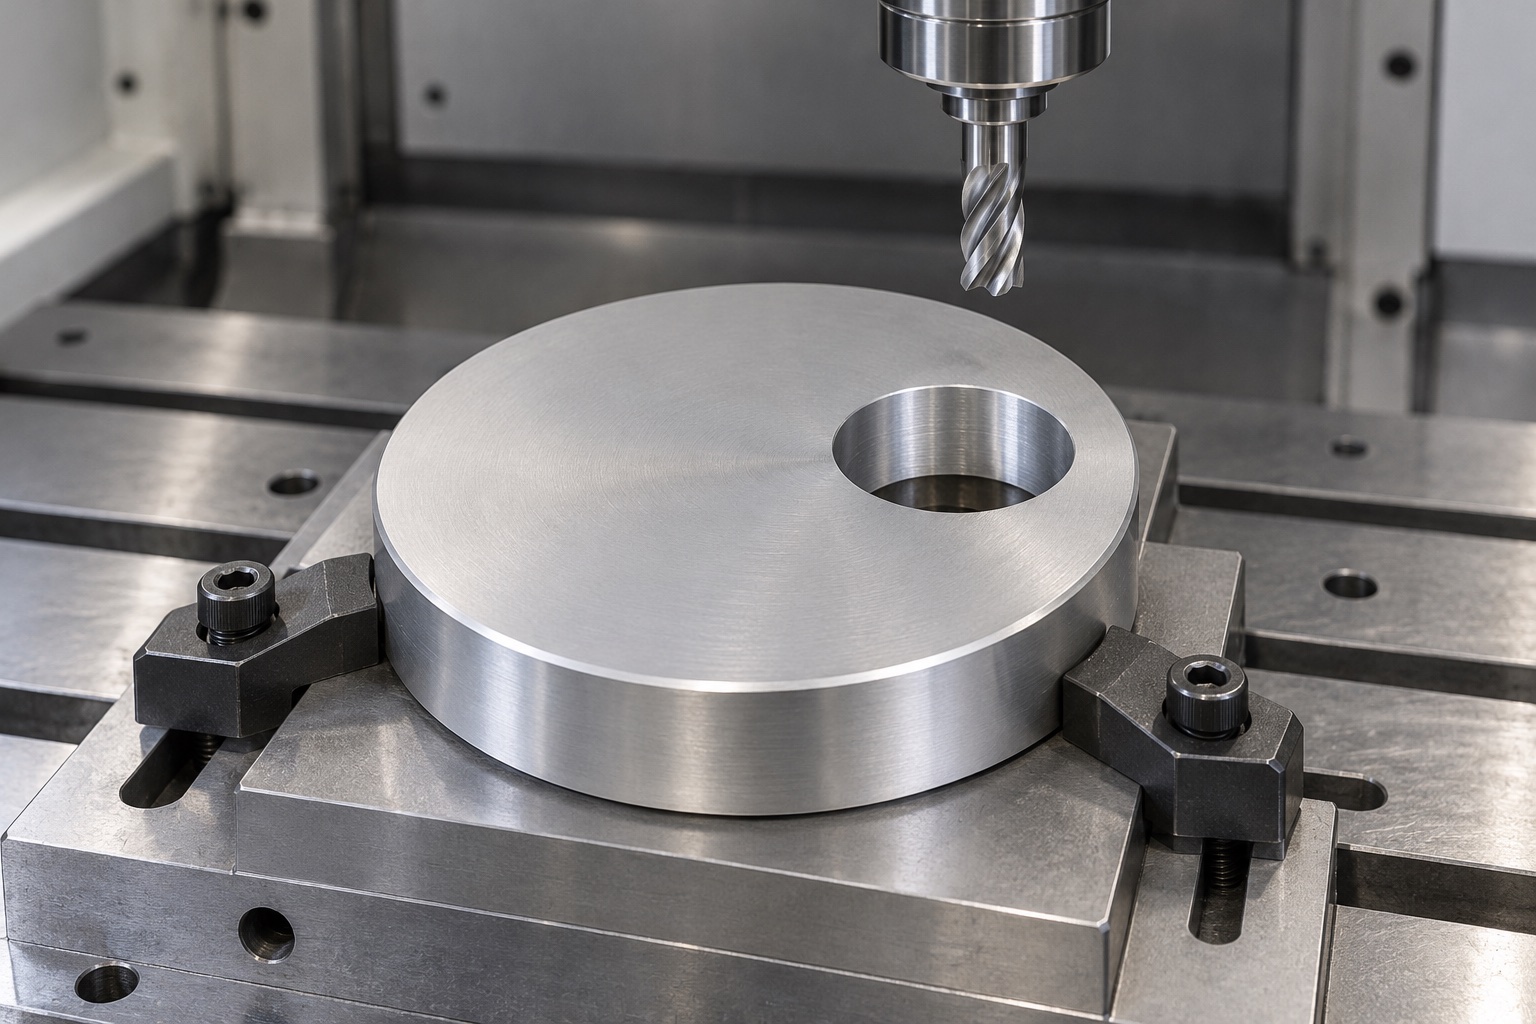
Identify the useful round exterior, permitted edge breaks, thickness and opposing face relationships. Clarify which regions contact the mechanism and which provide clearance. The surrounding contact must not be inferred from a photograph of a smooth aluminum rim. An outside micrometer reading addresses selected size, not every form or relation between the two axes. If the actual application needs defined contact pressure, stiffness or resistance to movement, those belong to its separate engineering and verification. Do not use mounting force to conceal a distorted disc and call the component dimensionally conforming.
Specify material and processing without transferring ratings
State the approved 6061 grade, stock condition, form, lot evidence and purchased final treatment. The illustrated silver surface does not select an anodized or untreated state. Review operations affecting bore clearance, face contacts or the exterior and include relevant final checks. Preserve identity through turning, offset machining and dispatch. Material records identify supplied stock within their scope; they do not establish wear life, validated cleaning, biological compatibility, sterile supply or medical certification. A commercially rated cam or an unrelated adjustment component does not transfer its performance merely because both parts are aluminum and appear circular.
Preserve references across concentric and offset operations
Plan how the outside profile, faces and offset bore remain related when the component is repositioned. Protect useful surfaces and remove chips before reorientation. Review tool access and the narrowest remaining section around the opening. Carr Lane's engineering resources provide general locating and clamping background, not a validated fixture recipe for this custom disc. Intermediate checks may assist process development, but final acceptance addresses the agreed finished condition. No universal clamp force, tool size or achieved eccentric tolerance is specified. A fixture-imposed relation should not replace the controlled drawing or a complete final inspection plan.
Finish boundaries without changing the offset envelope
Inspect bore entries, face edges and the round contact perimeter for attached material or unintended sharp features. Apply approved edge requirements while preserving useful contact and the actual mounting definition. Hand polishing the rim to make one assembly move more easily can alter geometry and requires controlled review. Cleaning should follow the purchased scope. A bright surface does not demonstrate low particles, validated disinfection or sterile delivery. Where residue, finish or contact appearance matters, agree relevant methods and evidence for the real material and equipment environment rather than relying on an illustrative machining or inspection photograph.
Inspect sizes and relationships as separate characteristics
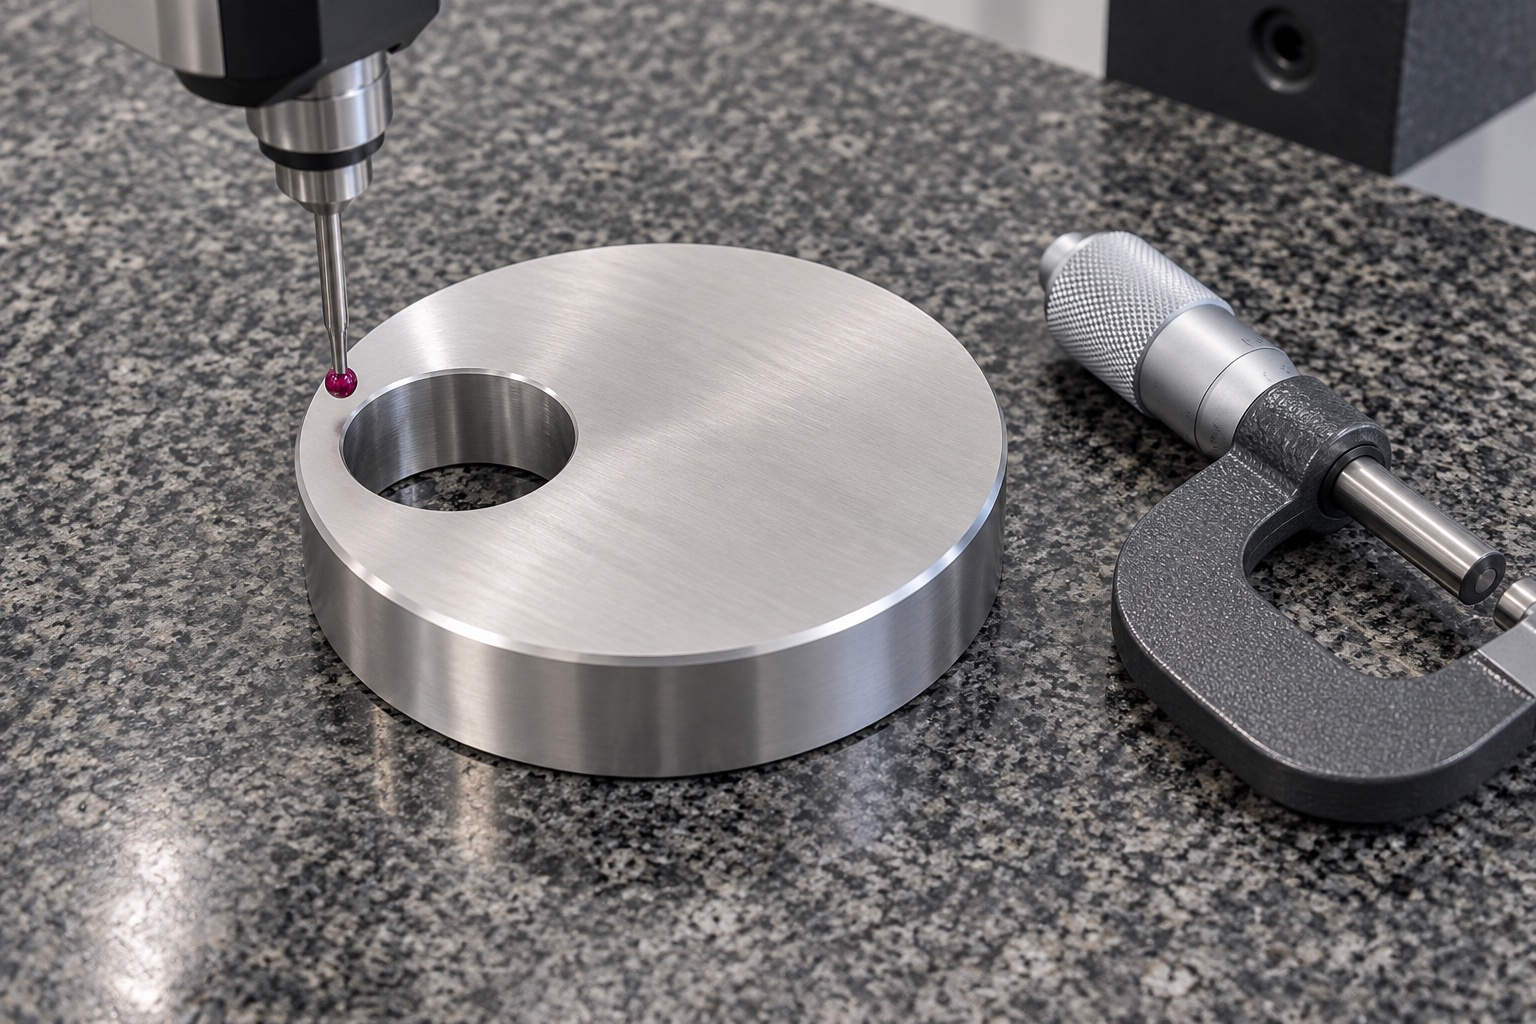
Map bore, exterior, finished thickness, face relationships and the specified offset to accessible methods. Agree the reference scheme, support and final treatment before acceptance. Checking the two diameters independently does not establish their relative position. A pin in the opening cannot verify the whole disc or its contact perimeter. A real report should identify revision, material lot, numbered characteristics, methods and actual observations. A CMM image depicts a possible arrangement, not a measured offset, achieved tolerance or calibrated adjustment result. Keep component geometry inspection separate from fitting the actual equipment mechanism.
Limit an optional adjustment observation
A separately agreed trial may examine mounting, seating, intended rotation, contact and access with identified disc, mounting member, support and mechanism revisions. Record the installed orientation, procedure and separate holding arrangement. Easy rotation does not establish load capacity, positional stability, resistance to vibration or repeatable settings. Those require separately defined evaluation of the complete real assembly and conditions. Distinguish trial discs from accepted production. Unexpected interference should trigger review before altering the rim, bore or mounting hardware simply to obtain a favorable demonstration or treating a hand-modified disc as a general production master.
Protect the accepted perimeter and variant identity
Separate finished discs so adjacent parts and loose hardware cannot strike the bore, useful rim or face contacts. Select supports that avoid bending or marking the accepted geometry. Keep lot, revision, final processing and inspection status with the shipment. Mechanical protective packaging does not imply sterile delivery. Receiving personnel should distinguish visually similar discs with different bore positions, thicknesses or diameters before installation. Preserve approved variant identity rather than rely on an unapproved handwritten setting mark, while leaving the equipment team's independent holding, motion and service qualification as a separate application responsibility.
Prepare an offset-specific manufacturing inquiry
Provide the controlled model and drawing, both axis definitions, mounting member, contact geometry, permitted settings, rotation envelope, retention method, useful faces, material, final processes and inspection deliverables. Separate optional assembly observations from holding and adjustment performance qualification. Review changed contacts, supports or mounting procedures before repeating manufacture. Approved prototype adjustments must enter revised documents rather than remain in a polished trial disc. This establishes a traceable CNC supply project without inventing measured adjustment results or confusing a dimensionally accepted eccentric component with a universally qualified medical instrument positioning or safety system.
Manufacturer background reference: www.carrlane.com.
FAQ
Do the bore and outside diameters define eccentricity?
Not by themselves. Their relative axis position needs an explicit controlled requirement and an agreed inspection method. A visibly off-center photograph is not an approved offset or a measurement record. Keep each size check distinct from the relationship between the two axes.
Does the disc hold its own angular setting?
No independent locking function is shown. The actual assembly must define mounting, axial retention and any method that holds the adjustment. A plain bore and easy rotation do not demonstrate positional stability, resistance to vibration or safe behavior during service.
Can the offset be treated as a universal travel value?
No. Useful movement depends on installed orientation, mating contact and permitted rotation. Review the complete mechanism and its interference envelope. The illustrated shape does not establish adjustment range, resolution, contact force or a calibrated relationship for every medical equipment installation.
May the supplier add a keyway or a setting mark?
Only as an authorized feature reflected in controlled documents and relevant inspection. Do not invent an unshown mounting or orientation method. The equipment designer must define those decisions rather than rely on a supplier modifying a disc to make one sample assembly work.
Does 6061 imply a rated cam or validated cleaning?
No. Material identity does not transfer another product's wear, load or locking ratings, nor establish the finished component's cleaning qualification or sterile status. Define relevant requirements and evidence for the actual grade, processing, contacts and equipment environment separately.
What should a repeat order review?
Review axis offset, bore and exterior geometry, face contacts, mounting arrangement, permitted settings, retention, grade and final treatment. Incorporate approved adjustments into controlled revisions. A manually polished disc or a favorable assembly photograph should not become an undocumented production reference.
tanghangyun@oemach.com