
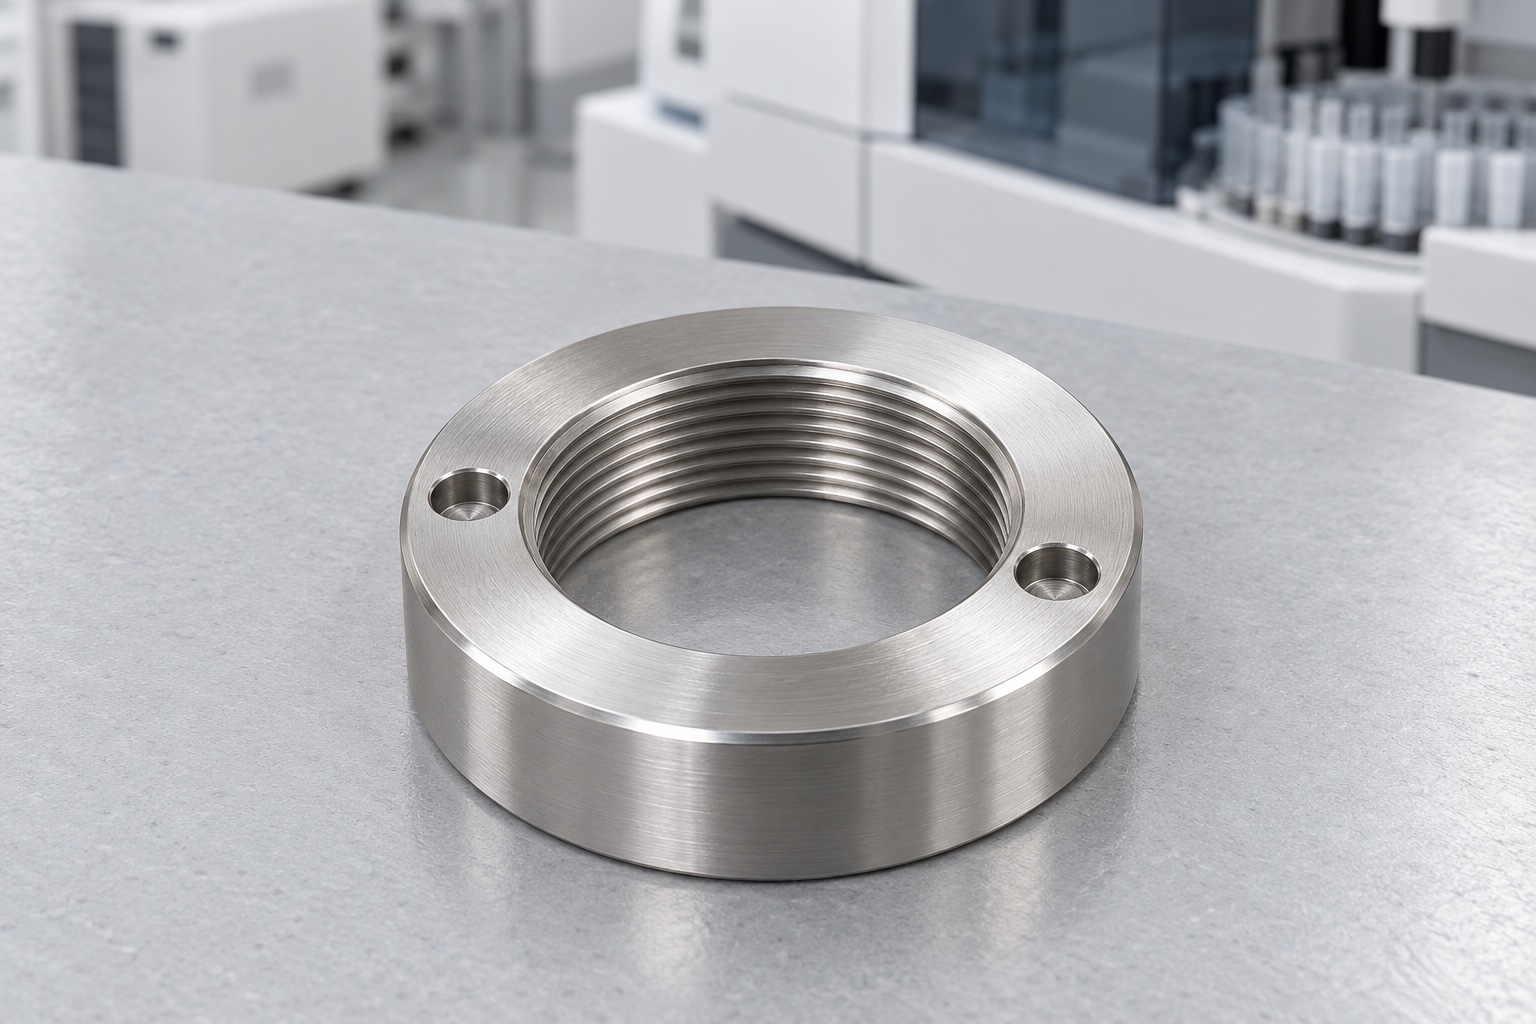
Representative proposed round retaining nut
This representative example describes a proposed one-piece 316L stainless steel retaining nut for an equipment-side threaded module sleeve in a medical instrument. The illustrative annular disc has a smooth cylindrical exterior, internal through-thread, flat seating face and two opposed blind axial tool holes in the other face. It has no slots, split, external thread or separate locking element. No actual customer delivery or manufactured sample is described. No achieved tolerance, clamp force, loosening resistance, load result, sealing, sterile status, medical certification or validated equipment safety is claimed as an actual measured production outcome.

Review the complete module contact stack
The proposed order would start with the released nut drawing and model, actual mating sleeve, retained module, shoulder and spacers, tool, installation method and inspection scope. The supplier would clarify useful annular contacts and required engagement before selecting a route. Missing dimensions or contradictory requirements would be resolved before manufacture. A nut's similarity to a catalog fastener would not transfer another product's rating or locking behavior. Manufacturing review would remain separate from the equipment team's clamp-force, anti-loosening and application qualification of the complete medical instrument assembly under its actual operating conditions.
Retain the approved stainless material
The material package would identify the accepted 316L stock form, condition, lot evidence and purchased final processes. Blanks would remain linked to their material lot through turning, face-hole machining, finishing and shipment. Stock allowance and holding contacts would be reviewed before selecting the route. Similar silver appearance would not justify another alloy or claims copied from a different fastener. Material evidence would identify the component stock, not demonstrate measured corrosion resistance, galling behavior, quantified cleanliness or sterile supply. Any such application property would need its own agreed requirement and acceptance evidence.
Establish face and thread references
Initial operations would establish approved references for the annular seating face, internal thread and tool-hole pattern. The sequence would consider setup transfers, remaining material and the nut's released condition. The supplier would avoid accepting the ring only while distortion from the fixture made it appear conforming. Chips would be removed from locating contacts before reorientation. Intermediate checks could support route development, but final acceptance would address drawing relationships after relevant operations and purchased final processing. A convenient outside holding diameter would not silently become a substitute for the approved functional inspection references.
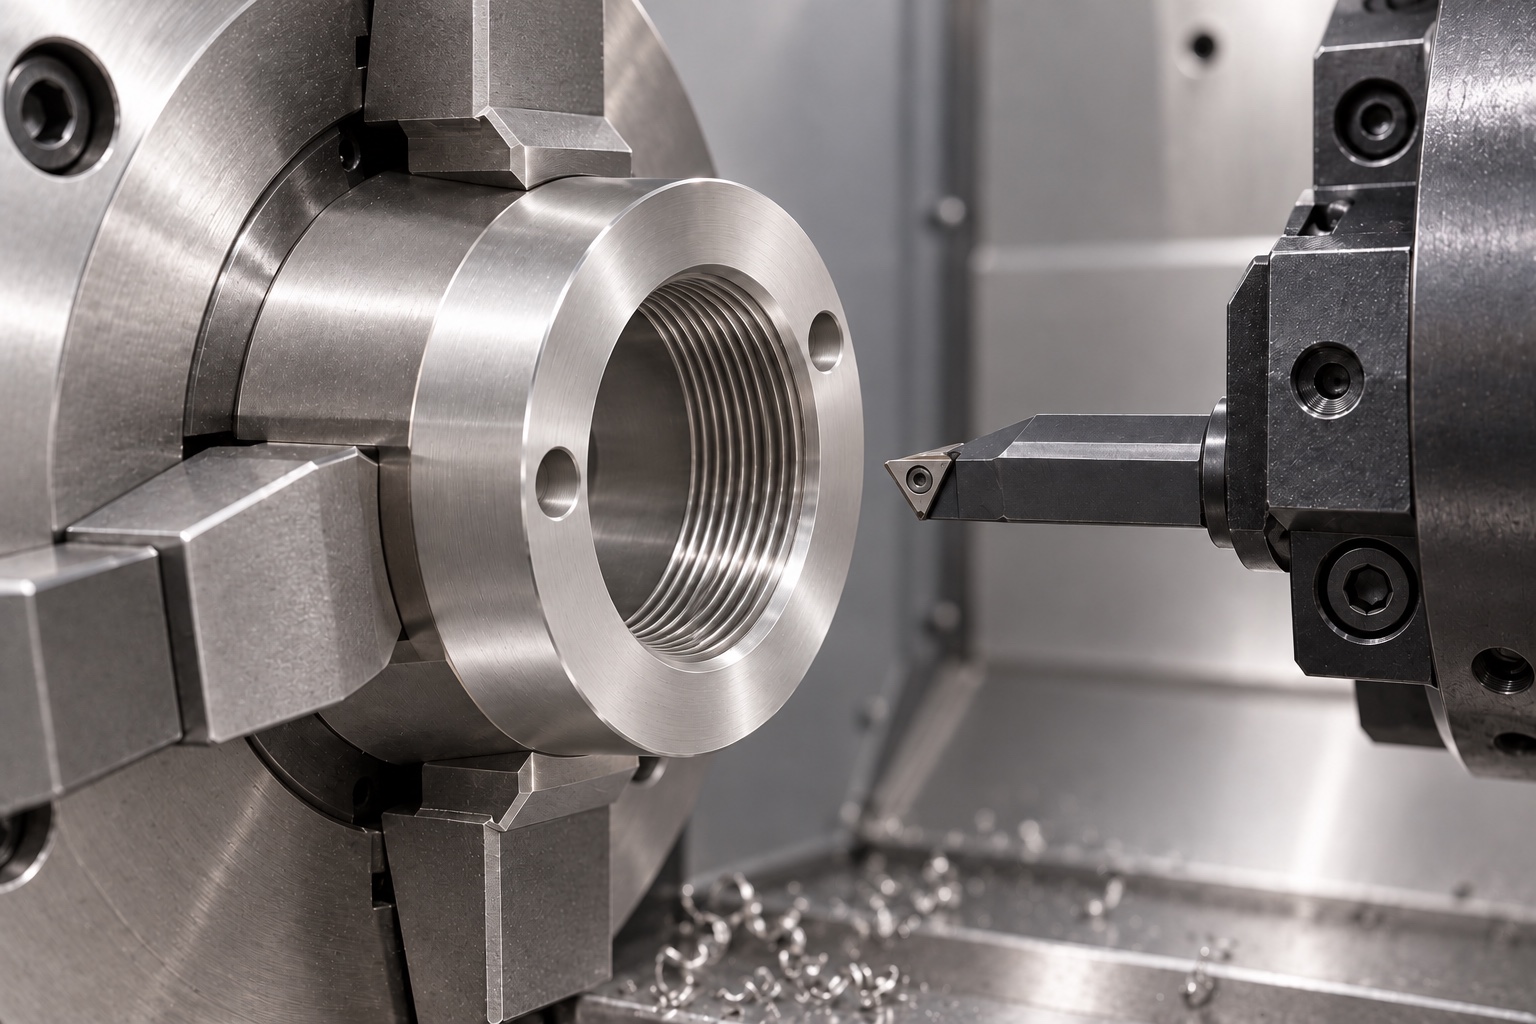
Machine the specified internal through-thread
The thread would follow the released system, size, pitch, direction, useful engagement and agreed acceptance criteria. Entry and runout regions would be reviewed before machining. Visible thread depth in the illustration would not define usable engagement. The supplier would not enlarge an entry, change the thread or shorten the nut merely to fit an unidentified sleeve. Authorized changes would enter controlled documents. A gauge observation would address its specified characteristics, not prove sufficient engagement, clamp force or loosening resistance in the complete nut, sleeve, shoulder and module stack used by the medical equipment team.
Preserve the useful annular seating face
Face size, thickness, permitted edge breaks and relationships to the thread would follow the approved contact definition. The supplier would distinguish useful contact from permitted entry relief or processing areas. Tool access and support would be reviewed before production. An informal spacer or polished relief would not be introduced to make one assembly seat favorably. Model and drawing conflicts would be clarified before cutting material. The retained face geometry would remain a component requirement, not evidence of sufficient clamping, a fluid seal or a qualified medical module attachment under actual service conditions.
Produce two defined blind tool holes
The two axial holes would follow approved diameter, spacing, depth, direction and reference relationships. Their blind form would not be replaced by through holes, radial features or slots for convenience. The supplier would review actual tool access without selecting a universal spanner from a concept photograph. Deeper drilling or a different drive interface would require authorization. Accepted changes would enter geometry and inspection documents, keeping subsequent nuts independent of an unidentified tool, hand-drilled specimen or undocumented installation practice that altered tool engagement or remaining annular material in the actual equipment assembly.
Finish and inspect the final interfaces
Finishing would examine thread entries and exits, tool-hole rims, annular edges and outer corners for attached material or unwanted sharp features. Released edge requirements would preserve engagement, seating and useful tool contact. Cleaning and final processing would follow the order with relevant finished-state checks. The inspection plan would identify methods, support and criteria for the thread, face, thickness, holes and reference relationships. A bright surface or favorable hand rotation would not replace these checks or demonstrate galling resistance, quantified particles, sterile delivery or validated medical equipment retention.
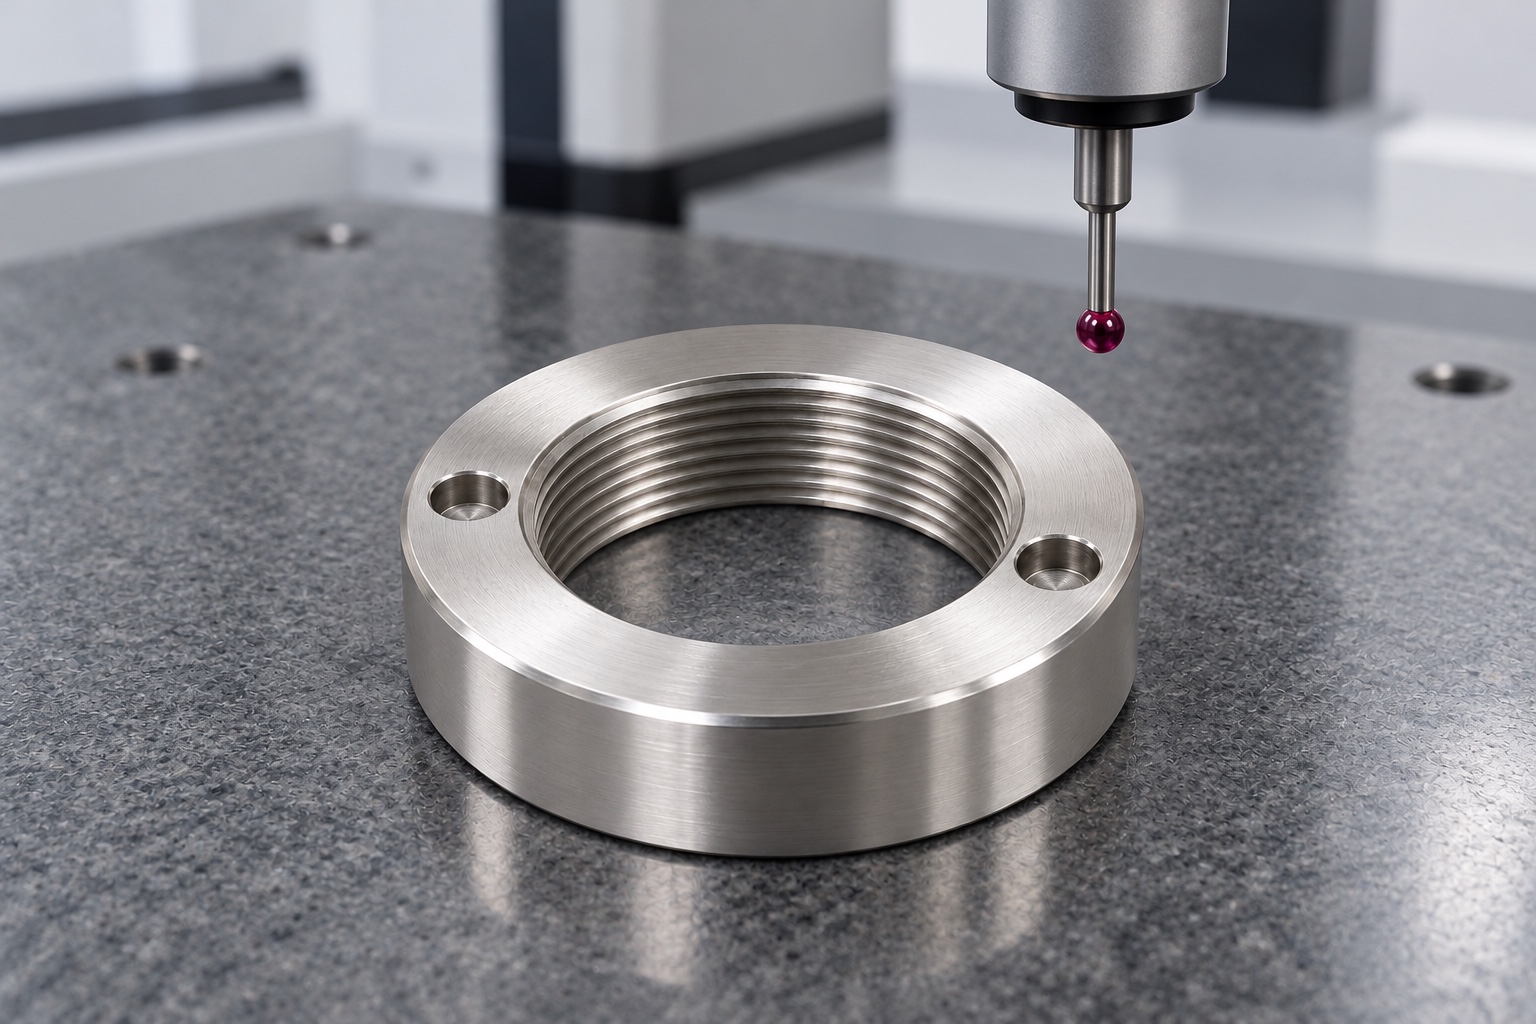
Prepare first-part records without invented results
The proposed report would identify drawing revision, material lot, numbered characteristics and agreed methods. No numerical values are supplied because this representative example has no manufactured sample or measurement record. Actual nonconformance and authorized changes would remain traceable. Component conformity would not establish clamp force, resistance to loosening, vibration performance or sealing. A thread gauge or inspection image would illustrate a possible method, not prove an achieved tolerance. The record would distinguish measured geometry from optional assembly observations and the equipment team's separate installation, retention and complete-application qualification.
Limit any optional installation observation
An agreed trial could examine thread entry, seating, engagement and tool access with identified nut, sleeve, module, spacer and spanner revisions. The approved installation procedure, lubricant and any separate retention components would be recorded. Unexpected interference would be reviewed before changing the nut or substituting a stack component. Successful hand assembly would not qualify torque, clamp force, anti-loosening behavior, fatigue or medical equipment safety. Trial nuts would remain separate from accepted production. Approved adjustments would enter revised documents rather than make one modified ring an informal gauge for other module configurations.
Protect threads, faces and tool-hole rims
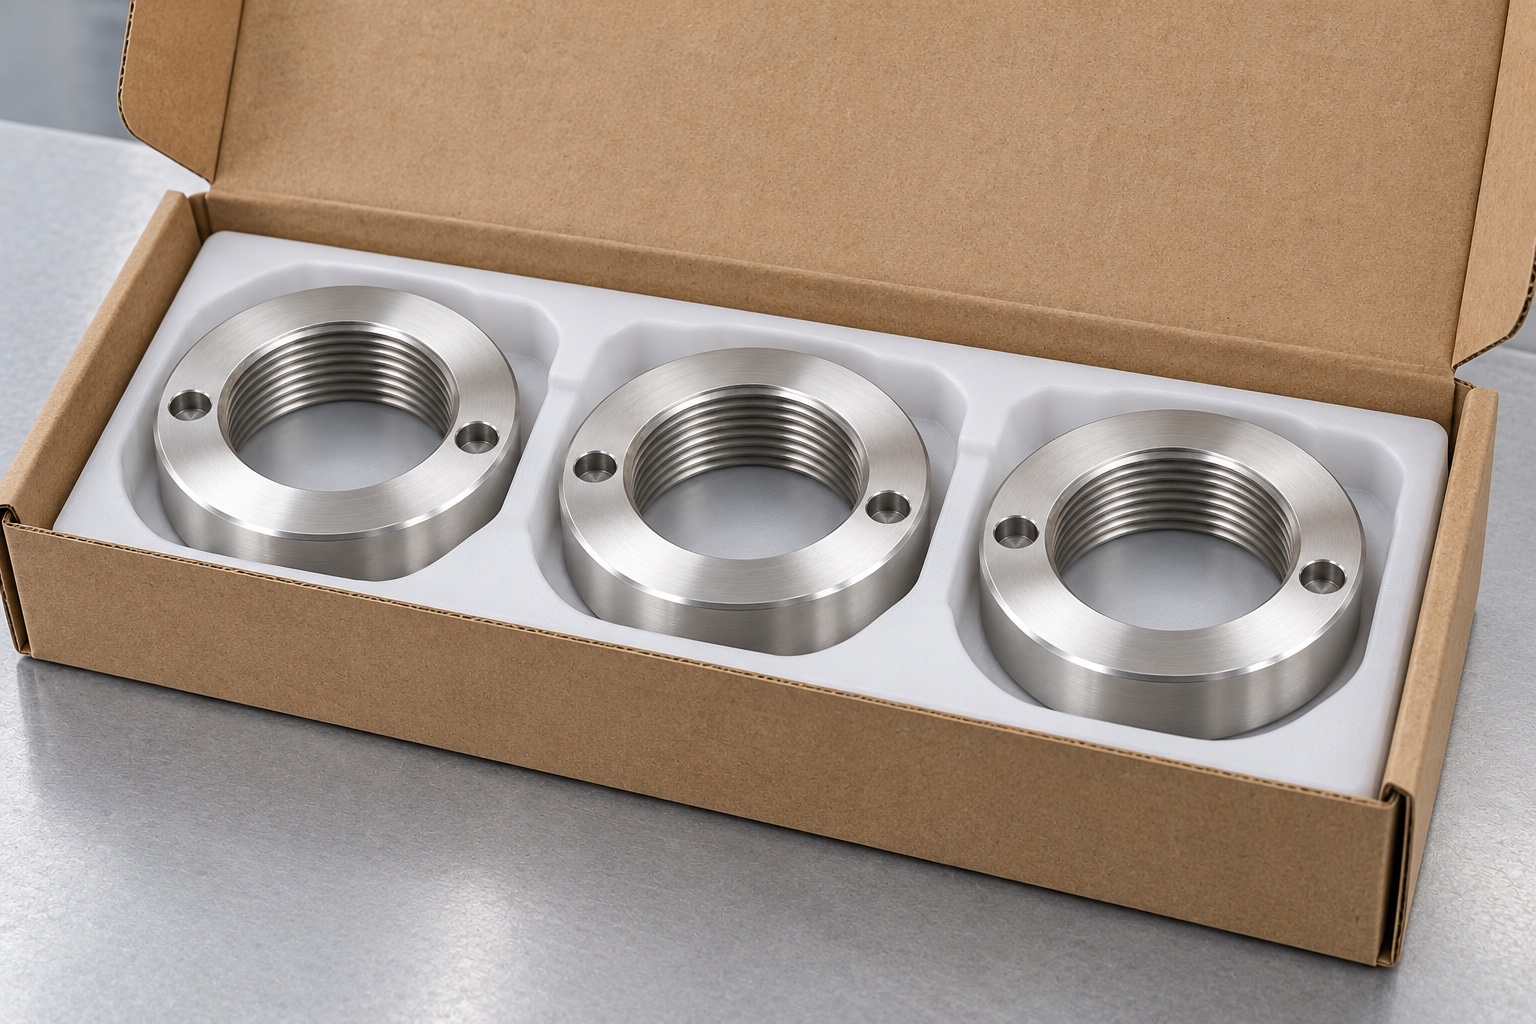
Finished nuts would be separated so hard hardware could not strike the internal thread entries, seating contacts or blind-hole edges. Packaging support would avoid distorting the annular section or introducing unapproved material onto accepted surfaces. Mechanical protection would not imply sterile delivery. Lot, revision, final treatment and inspection status would accompany the shipment. Receiving checks would distinguish thread direction, pitch, thickness and drive-pattern variants, prototypes and released production. These controls would preserve accepted component identity before approved installation and any separate retention, maintenance or cleaning evaluations by the medical equipment team.
Maintain a stack-specific production baseline
The final package would preserve the released geometry, actual sleeve and module stack, contact and engagement requirements, tool identity, installation access, material evidence, final process, inspection methods and packing scope. Approved prototype changes would become revised documents before repeat manufacture. Changes to sleeves, spacers, tools, lubricants or service conditions would trigger review. This representative workflow illustrates a traceable custom CNC project without inventing customer history, measured performance or self-locking behavior, and without confusing a conforming stainless retaining nut with a qualified seal or validated medical equipment module retention system.
Manufacturer background reference: www.gedore.com.
FAQ
Is this an actual delivered customer nut?
No. It is a representative proposed CNC workflow with illustrative component and process images. There is no customer delivery, manufactured sample, measurement record or achieved result. A real order would require its own released documents, production records and measured acceptance evidence.
Do the two tool holes provide locking?
No locking behavior is established. They provide a specified tool interface in this concept. Any anti-loosening or retention function would need its own approved design and qualification using the actual nut, sleeve, module stack, installation method and operating conditions.
Does the case specify a torque or clamp force?
No. No torque or clamp-force result is available. Those requirements belong to the actual approved assembly and procedure. Material identity, nut diameter, a tool illustration or successful hand rotation would not establish a universal installation value or qualified retention performance.
Why inspect the seating face as well as the thread?
They have different specified characteristics and functional relationships. A passing thread gauge does not automatically verify the useful annular face, thickness, tool holes or seating against the actual stack. The agreed dimensional plan would address each drawing requirement in the defined final condition.
Is this a fluid-sealing component?
No qualified sealing scope is provided. The proposed use is equipment-side module retention. Sealing, galling resistance, corrosion performance, quantified cleanliness or sterile supply would need separate defined and verified requirements, not assumptions based on a bright stainless ring.
What would be reviewed on another order?
Review sleeve thread, module and spacers, useful seating, engagement, tool and access, material, final process, lubricant and service conditions. Approved changes must enter controlled documents rather than rely on a manually adjusted ring or another equipment assembly's retention claims.
tanghangyun@oemach.com