
This article successfully disassembles the prototype into reproducible materials, equipment, tooling, procedures, tools, outsourcing and measurement conditions, and provides the first batch release and change trigger mechanism.
Mass production handover is not about copying the sample program to another machine tool; it is necessary to freeze the product and process versions, use formal resources to complete the first article and small batch verification, and then increase the volume based on the data. The specific process still needs to be combined with frozen drawings and BOM, materials and outsourcing sources, tooling program and tool versions, inspection plans, first article evidence, initial tightening control and change approval confirmation.
Typical problems, causes, controls and evidence
| Problem | Likely cause | Control action | Acceptance evidence |
|---|---|---|---|
| The sample is qualified but the first batch fluctuates greatly | Formal materials, equipment, tooling, tools or outsourcing are different from the prototype stage | Complete first article and small batch safe launch validation using volume production resources | Resource inventory, first article reports, and first trend data |
| Old procedures/drawings still used on site | Version distribution, old version recycling and change confirmation are not closed loops | Establish a unique version baseline and electronic/on-site sign-off mechanism | Version, program verification and change approval records |
| Abnormalities can only be recalled by the old master | Process knowledge and release basis have not formed a handover package | Curing routes, setups, tools, parameter windows and reaction plans | Process card, control plan, training and abnormal closed loop |
Freeze the product baseline first and then discuss handover
Models, 2D drawings, BOMs, materials, heat treatment, surface preparation and acceptance specifications must have consistent and traceable versions. Temporary relaxations during the trial assembly phase, manual repairs and acceptance of deviations are either converted into formal requirements or closed before series production. If the design still changes frequently, the disposal of work-in-progress and first-article re-production conditions should be clarified, and multiple versions cannot be mixed into the first batch.
Divide the sample process into reproducible resources
Prototypes may rely on experienced operators, multiple alignments, universal soft grippers, or temporary outsourcing. The handover package should specify the blank and supplier, equipment capabilities, tooling drawings, clamping direction, program verification values, tool list and life, parameter window, cleaning, packaging and outsourcing routes. Any “fine-tuning” sessions should be translated into steps, boundaries, and a response plan.
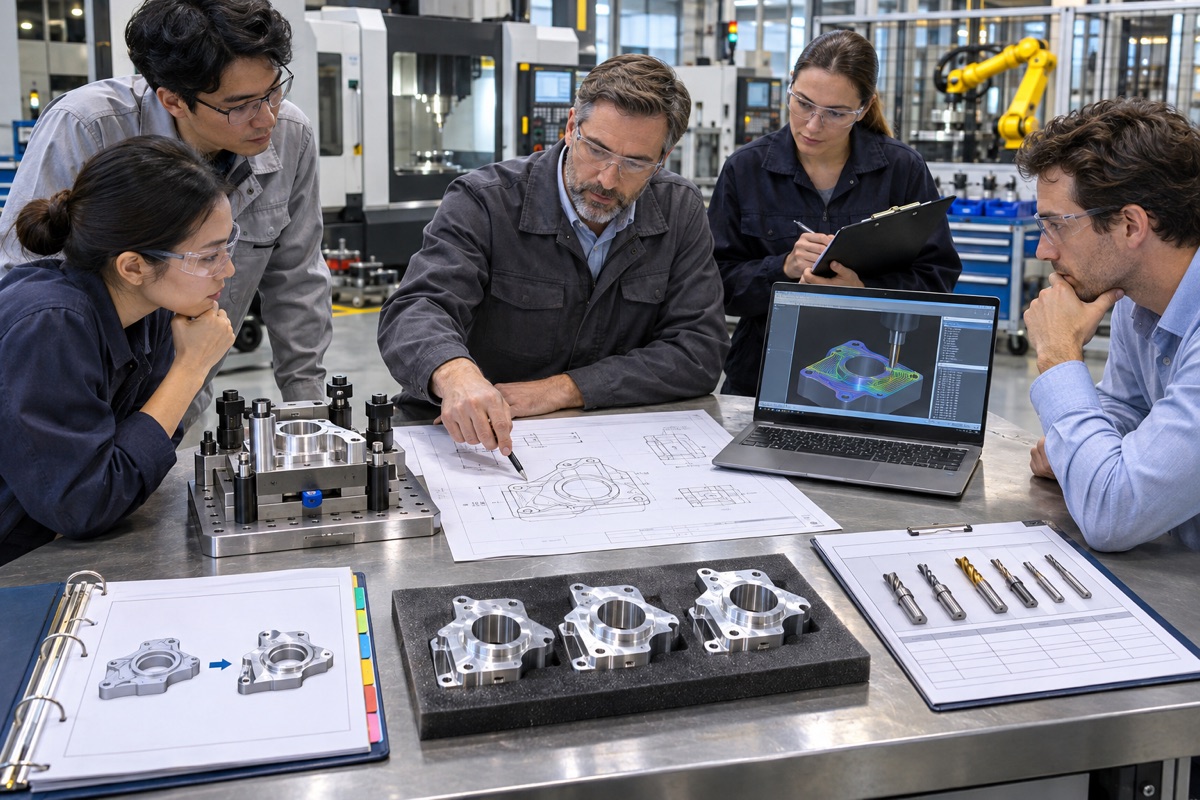
The handover package should freeze products, processes, resources and testing versions.
The inspection plan must correspond to the production process
Drawing characteristics should be mapped to processes and inspection methods, especially characteristics that cannot be measured again in the intermediate state. Measurement procedures, fixtures, temperatures, gage calibrations, and reporting templates should be version controlled. ISO guidance on documented information emphasizes the use of appropriate documentation to support the process and preserve evidence of results; the format can be flexible, but responsibilities, inputs, outputs and records cannot be missing.
The first article to be verified is the formal production process
The first piece is not selected from samples for retesting, but is manufactured and verified using planned mass production materials, equipment, tooling, procedures, tools, personnel and outsourcing routes. Although SAE AS9102 is oriented to aviation, its core idea has reference value: the first one is used to prove that the product implementation process is understood and that it can produce products that meet the design. Other industries should establish applicable methods based on customers and their own quality systems.
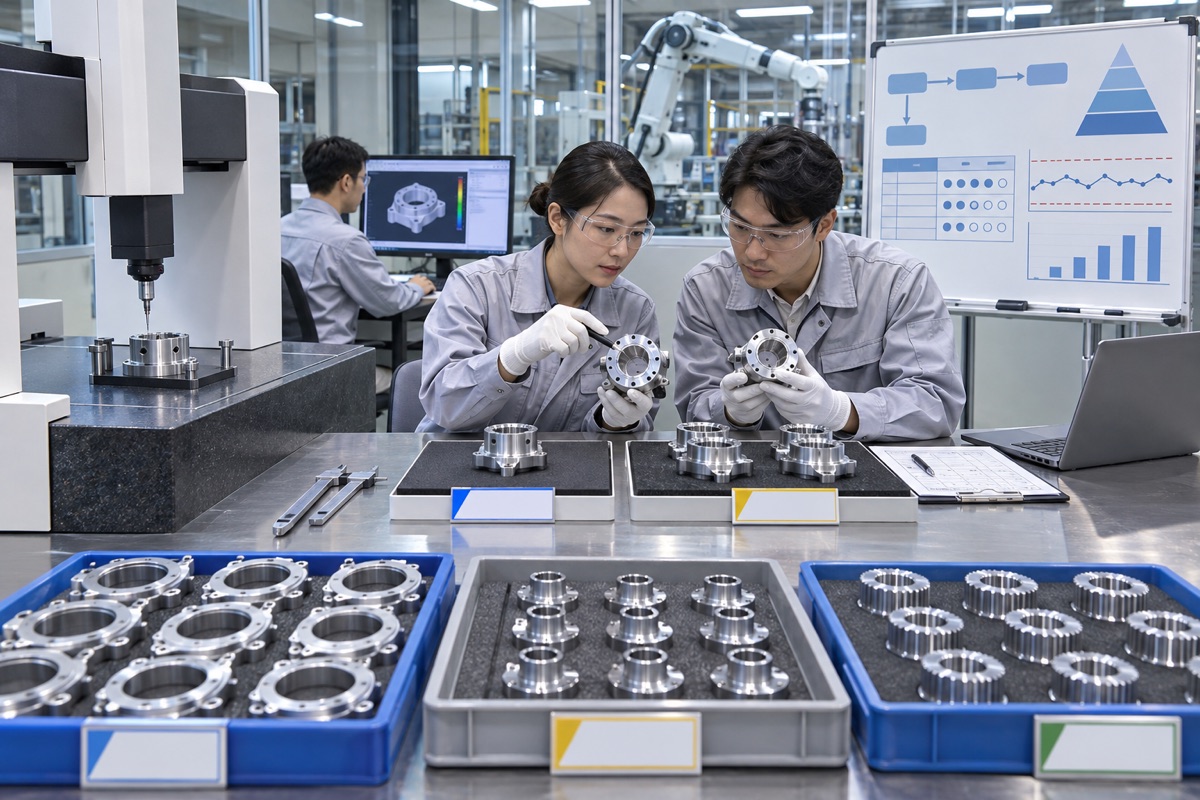
Use mass production resources to complete the first article and small batches and strictly monitor them before releasing the product.
The first batch needs to be strictly monitored rather than released immediately
From the first article to the stable batch, a small batch safety start-up stage can be set up: increase the frequency of key characteristic detection, monitor tool life, machine tool thermal status, tooling repeatability and outsourced fluctuations, and correlate part data with installed machine performance. The control plan must specify exception triggering, isolation, review and release authority, and cannot just state "rework beyond tolerance".
Change triggers re-approval and continuous review
Changes in design, materials, suppliers, equipment, tooling, procedures, tooling, measurements, or outsourcing can invalidate the first article basis. The quality system should define when partial or complete first articles are required. Problems in the early stages of mass production should be written back to drawings, PFMEA/risk lists, process cards and control plans so that the next batch uses the same knowledge baseline instead of relying on personal memory.
Summary
Mass production handover is not about copying the sample program to another machine tool; it is necessary to freeze the product and process versions, use formal resources to complete the first article and small batch verification, and then increase the volume based on the data. The specific process still needs to be combined with frozen drawings and BOM, materials and outsourcing sources, tooling program and tool versions, inspection plans, first article evidence, initial tightening control and change approval confirmation.
FAQ
Can I place a large order directly after the sample is qualified?
Not recommended. Formal resources and processes should be confirmed first, and first article and small batch stability verification should be completed.
Does the first article require only a full size report?
Full dimensions are an important part, as well as proof that materials, workmanship, outsourcing and records are performed to the approved version.
Is it necessary to replace the machine with a new one?
Determined by risk, customer and quality system; at a minimum the impact of equipment changes on critical characteristics should be assessed and approval documented.
Ready to get a quote for your CNC machined parts?
Submit your engineering drawings to qiancj@oemach.com. We support prototype sampling and small-batch production with strict tolerance control.