
HRA 90 is not a complete machining specification. Binder content, grain size, carbide type, density, toughness, conductivity and sintering state can differ at similar hardness.
Fully sintered cemented carbide combines high hardness and abrasion with limited toughness. Conventional milling may have narrow specialist windows, but diamond grinding and qualified alternative processes are more common.
Carbide route risks and controls
| Risk | Control | Evidence |
|---|---|---|
| Very short mill life and edge chipping | Stop applying steel parameters; review grinding or alternatives | Grade, life and surface record |
| EDM creates functional risk | Specify finishing and integrity inspection | EDM settings and layer evidence |
| Route chosen only from HRA | Review binder, grain, conductivity and geometry | Material certificate and trial approval |
Obtain the full carbide grade
Request grade designation, composition, cobalt or other binder content, grain size, density, toughness, conductivity and sintered state. Two grades near HRA 90 can respond differently, so hardness alone is insufficient for quoting or process approval.
Understand conventional milling limits
Ordinary carbide tools can wear or chip rapidly against fully sintered carbide, while the workpiece may edge-chip. Specialized tools and very small allowances can sometimes work, but cost, stability and surface integrity require representative trials rather than transferred hardened-steel practice.
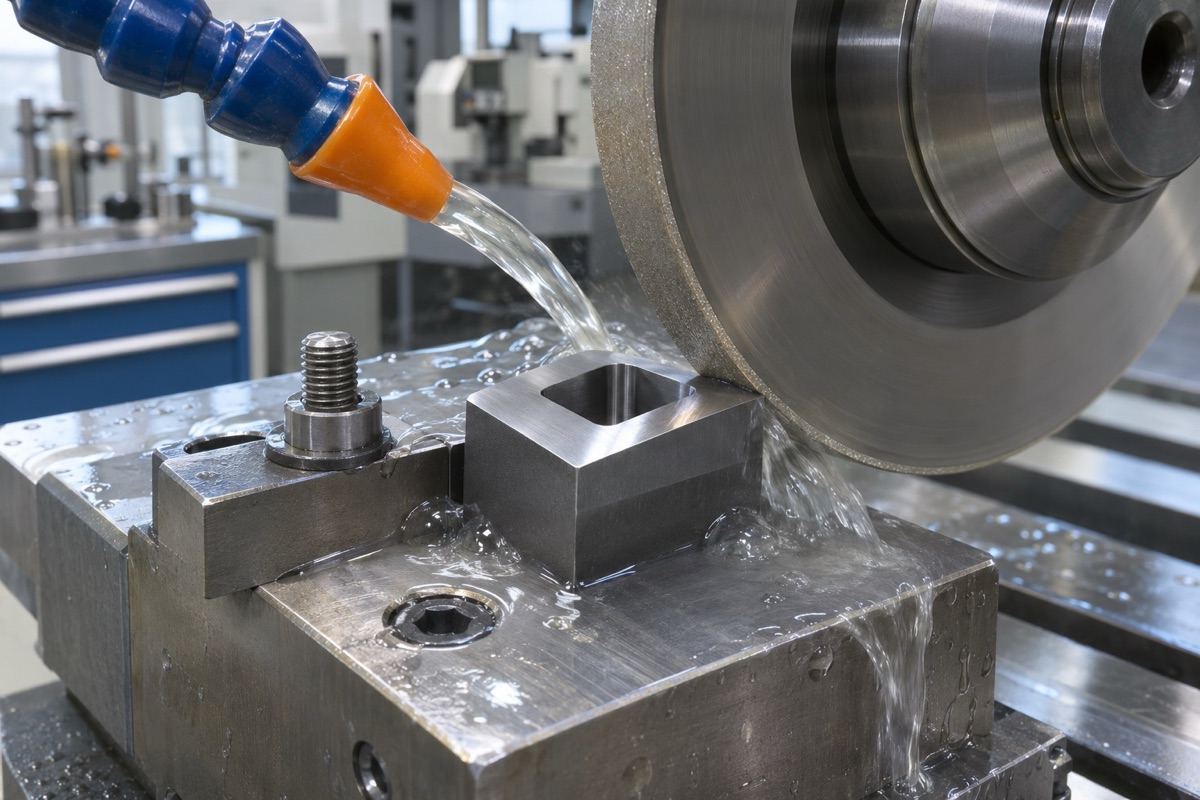
Fully sintered carbide commonly reaches final geometry through controlled diamond grinding.
Choose grinding, EDM or other qualified routes
Diamond grinding is common for faces, diameters, bores and profiles. Conductive grades may use sinker or wire EDM for slots and contours, but recast layers, thermal effects and microcracks may require grinding or polishing. Laser and pre-sinter shaping have separate heat and shrinkage limits.
Select for function and total cost
Wheel access, inside corners, stock removal, electrode or tool consumption, cycle time, rework and inspection all affect the route. First articles should link material batch and process settings with dimensions, edges and surface-integrity evidence before production is frozen.
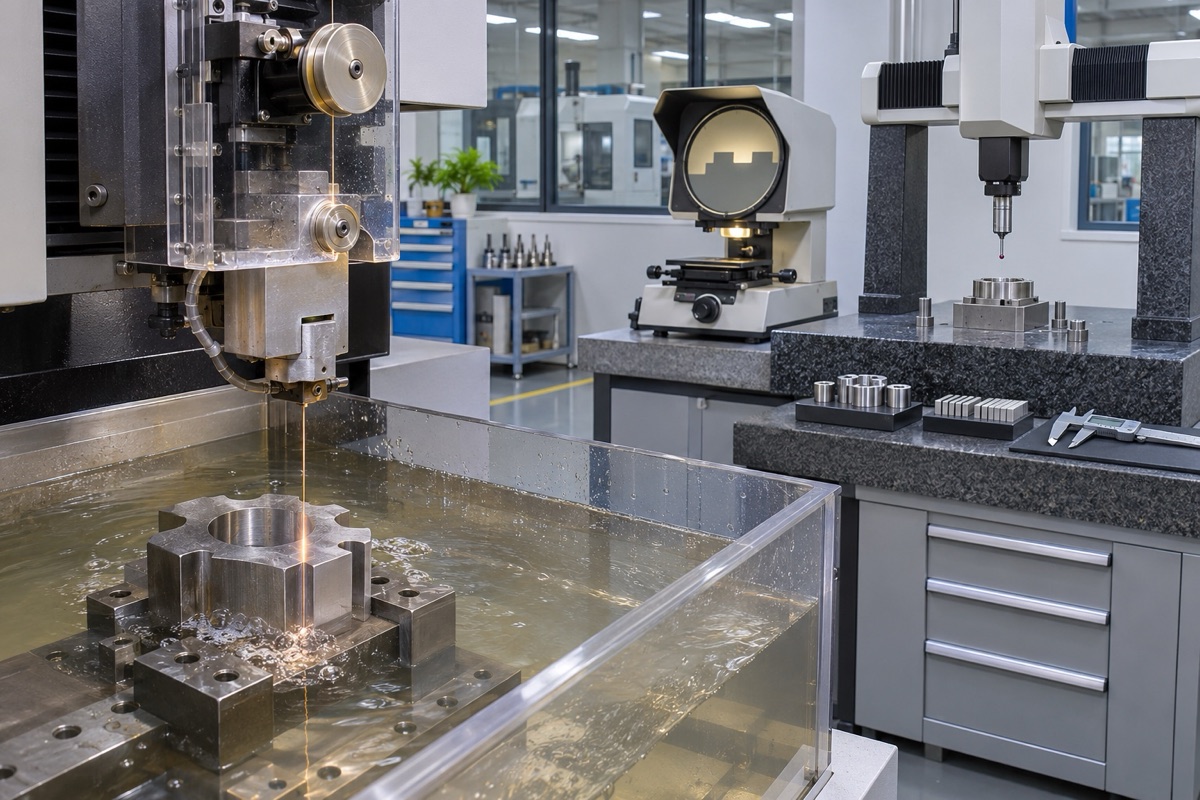
Conductive grades may use EDM, followed by evaluation of the recast and heat-affected layer.
Summary
HRA 90 does not define machinability; full grade data and functional requirements determine whether diamond grinding, EDM, laser, pre-sinter shaping or a proven specialist milling window is appropriate.
FAQ
Is HRA 90 carbide absolutely impossible to mill?
No, but conventional milling is usually high-risk and inefficient and needs specialist validation.
Can every carbide grade be wire cut?
No. Sufficient conductivity and acceptable thermal surface effects must be confirmed.
Can grinding damage carbide?
Yes. Poor wheel condition, cooling or load can cause heat damage, cracks or chips.
Ready to get a quote for your CNC machined parts?
Submit your engineering drawings to qiancj@oemach.com. We support prototype sampling and small-batch production with strict tolerance control.