
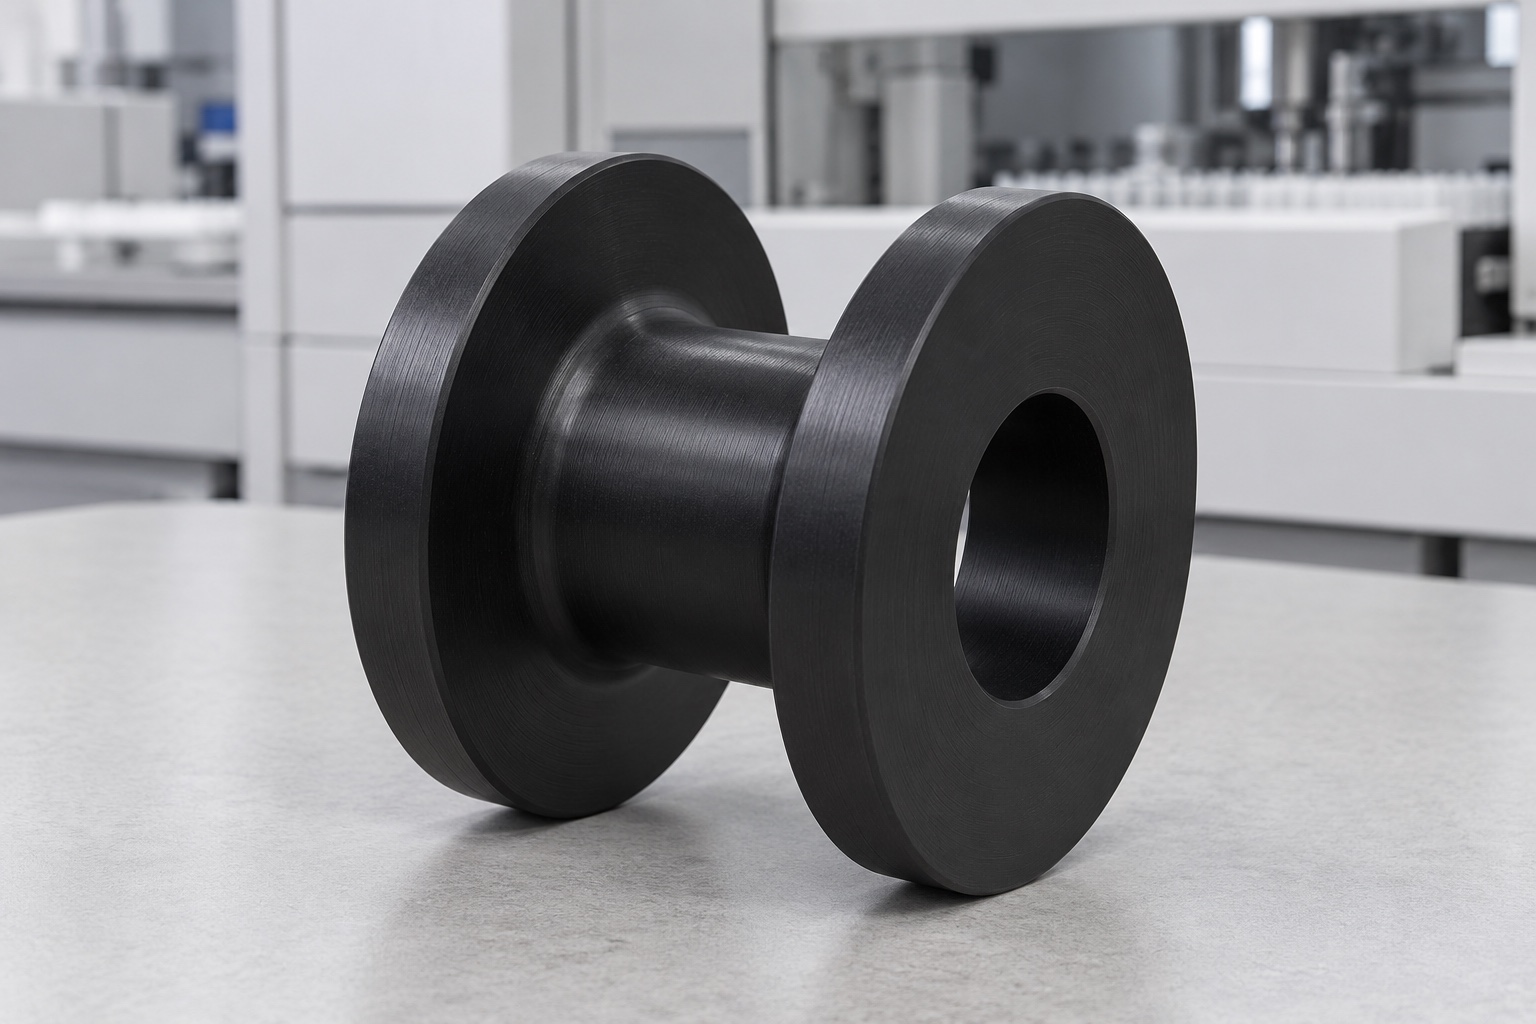
Representative proposed stationary cable guide
This representative example considers a proposed one-piece black POM spool used as a stationary cable-contact guide in a medical equipment service route. Its illustrative geometry has two equal circular flanges, a smaller cylindrical waist and one plain coaxial through-bore. No cable, bearing, rotating support or fluid path is illustrated. It is not an actual customer delivery or measured component. No achieved tolerance, cable life, abrasion result, electrical performance, strain-relief capacity, sterile status, medical certification or validated equipment performance is claimed as a measured production outcome.

Review the cable and mounting configuration
The proposed order would begin with controlled spool geometry, exact cable and connector information, the applicable bend requirement, intended contact regions, mounting hardware, service access and inspection scope. The supplier would clarify the waist contact and flange boundaries before turning. A general cable guidance reference would be background rather than approval of the custom guide. Missing conditions or model conflicts would be resolved before manufacture. CNC review would remain separate from the equipment team's electrical, cable-life and application evaluation of the complete medical instrument route and actual operating conditions.
Retain the approved POM grade
The material package would specify the accepted POM grade, stock form, lot evidence and final processing. Blanks would remain traceable through turning, finishing and packing. Black appearance would not justify substitution of another polymer or modified grade. Stock allowance and gripping regions would be reviewed before selecting the route. Material documentation would identify the purchased stock, not establish electrical insulation, flame behavior, jacket compatibility or quantified cleanliness of the finished spool. Any such properties would need their own agreed requirements and evidence within the actual equipment application.
Plan the bore and contact references
Initial operations would establish approved holding and reference features used to relate the bore, waist and flanges. The supplier would consider setup transfer and the component's unclamped condition instead of relying only on convenient raw surfaces. Excessive restraint that distorted a flange or waist would be avoided. Chips would be controlled before reorientation. Intermediate dimensions could support process development, but final acceptance would address the agreed conditioned and finished state after relevant operations and purchased final processing. Useful contact and mounting regions would remain identifiable throughout the proposed route.
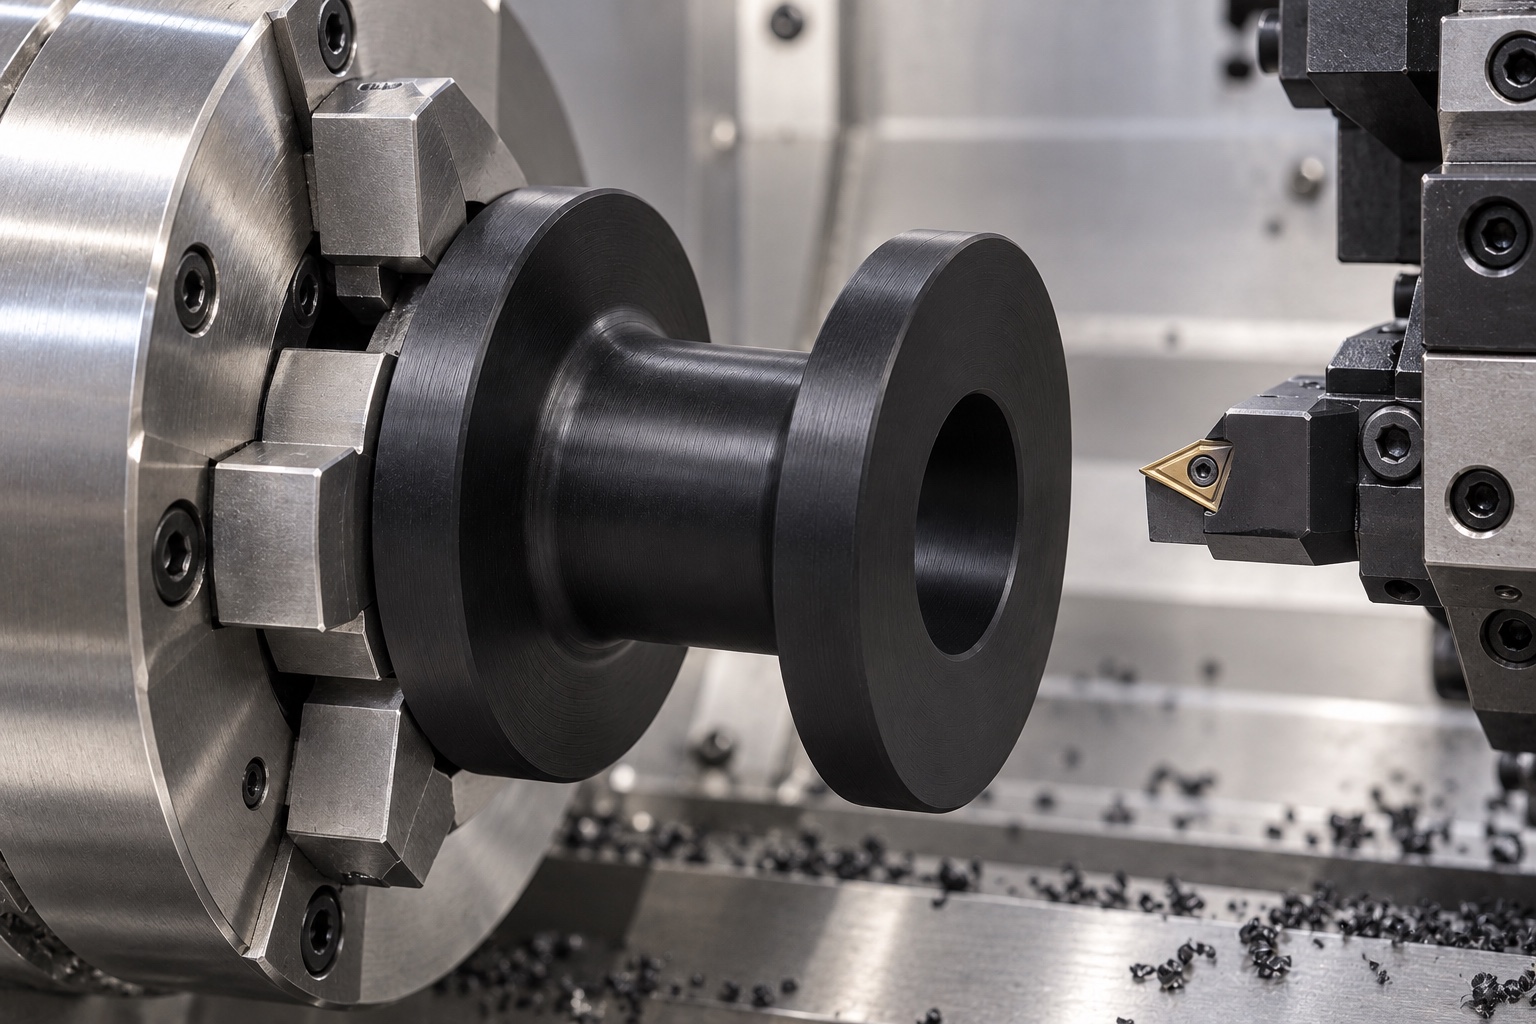
Turn the defined cylindrical waist
The waist would follow approved contact size, useful width, form and transition requirements. The actual cable radius definition would be reviewed by the responsible designer before it was converted into component geometry. The supplier would not select a universal ratio from cable diameter or reduce the waist merely to fit an unidentified route. Authorized changes would enter controlled documents. The turned region would remain a specified mechanical contact surface, not evidence of adequate jacket life, conductor integrity, signal performance or safe repeated motion in the complete medical equipment cable arrangement.
Machine the two flange boundaries
Flange size, separation, inner faces, root radii and edge requirements would follow the approved drawing and cable-contact definition. Tool access and remaining material would be reviewed before production. The supplier would not add an informal slot or thin a flange to pass a connector. Model conflicts would be clarified before cutting material. Changes would remain traceable so later orders did not depend on a hand-trimmed specimen, altered connector or undocumented routing practice. The controlled flange geometry would be distinct from evaluation of pinch, rubbing and service access in the actual enclosure.
Preserve the stationary mounting arrangement
The plain bore, seating faces and any approved mounting contacts would follow released dimensions and installation requirements. No bearing, sleeve, thread or improvised washer would be inferred from the concept. The supplier would review how the actual attachment affected component support, without defining a rotating function. Changes in mounting would require authorization before the guide was used as a trial assembly. A central hole and favorable fit would not independently establish retention, strain relief or permissible installation compression in an unspecified medical instrument cable route and support configuration.
Finish and inspect the contact condition
Finishing would examine waist, roots, flange edges and bore entries for attached material or unwanted sharp features. It would preserve approved contact size and inner spacing. Cleaning would follow the purchased polymer-compatible scope with relevant finished-state checks. The dimensional plan would define conditioning, support and measurement contact for the required waist, flanges, bore and reference relationships. A smooth appearance or favorable cable fit would not replace those checks or establish low abrasion, quantified particles, validated cleaning or sterile delivery. Ambiguous requirements would be resolved before production.
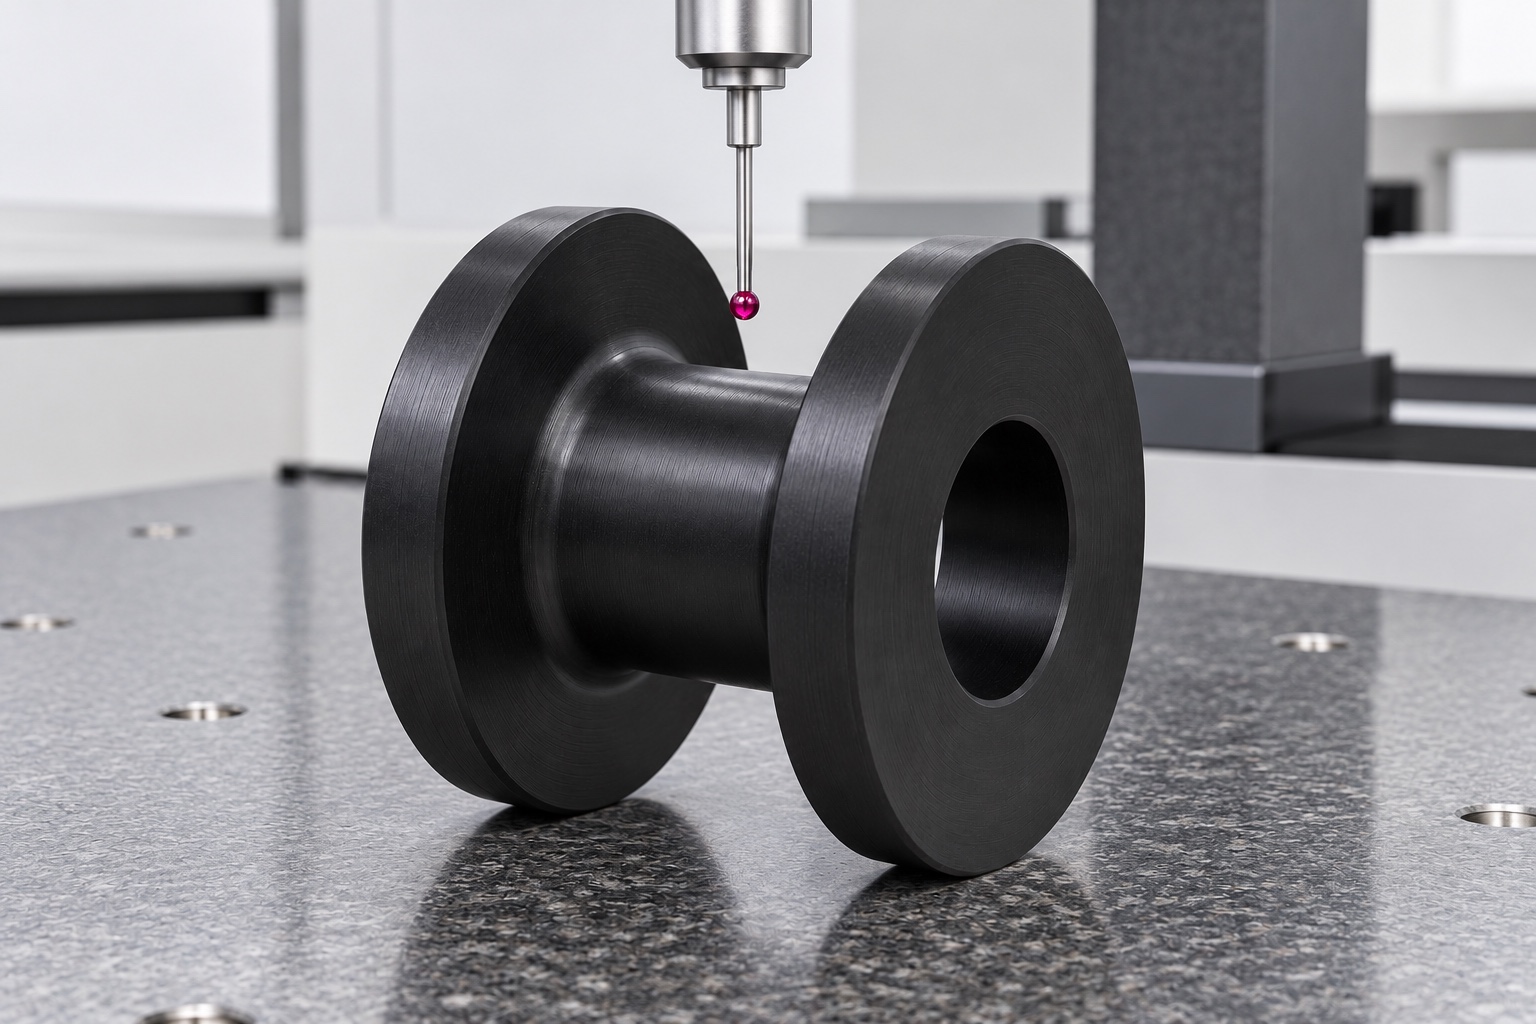
Prepare first-part scope without results
The proposed first-part package would identify drawing revision, polymer lot, numbered characteristics and agreed methods. No numerical results are supplied because there is no manufactured sample or measurement record for this representative example. Actual nonconformance and authorized changes would remain traceable. Component conformity would not demonstrate cable life, electrical performance or strain-relief capacity. A lathe or inspection illustration would not prove an achieved tolerance. The report would distinguish measured geometry from an optional static route observation and independent cable or complete-equipment qualification for the actual operating conditions.
Define a limited static route observation
An agreed trial could examine installation, connector passage, approach and exit, intended cable contact and service access with identified cable, guide and mounting revisions. The mounting method and applicable bend requirement would be recorded. Unexpected rubbing or pinch contact would be reviewed before modifying the spool. Favorable static fit would not qualify abrasion life, conductor integrity, signal quality or repeated-motion suitability. Trial guides would remain distinct from accepted production. Approved adjustments would enter revised documents rather than turn a hand-trimmed spool into a general gauge for other cable routes.
Protect waist and flange roots
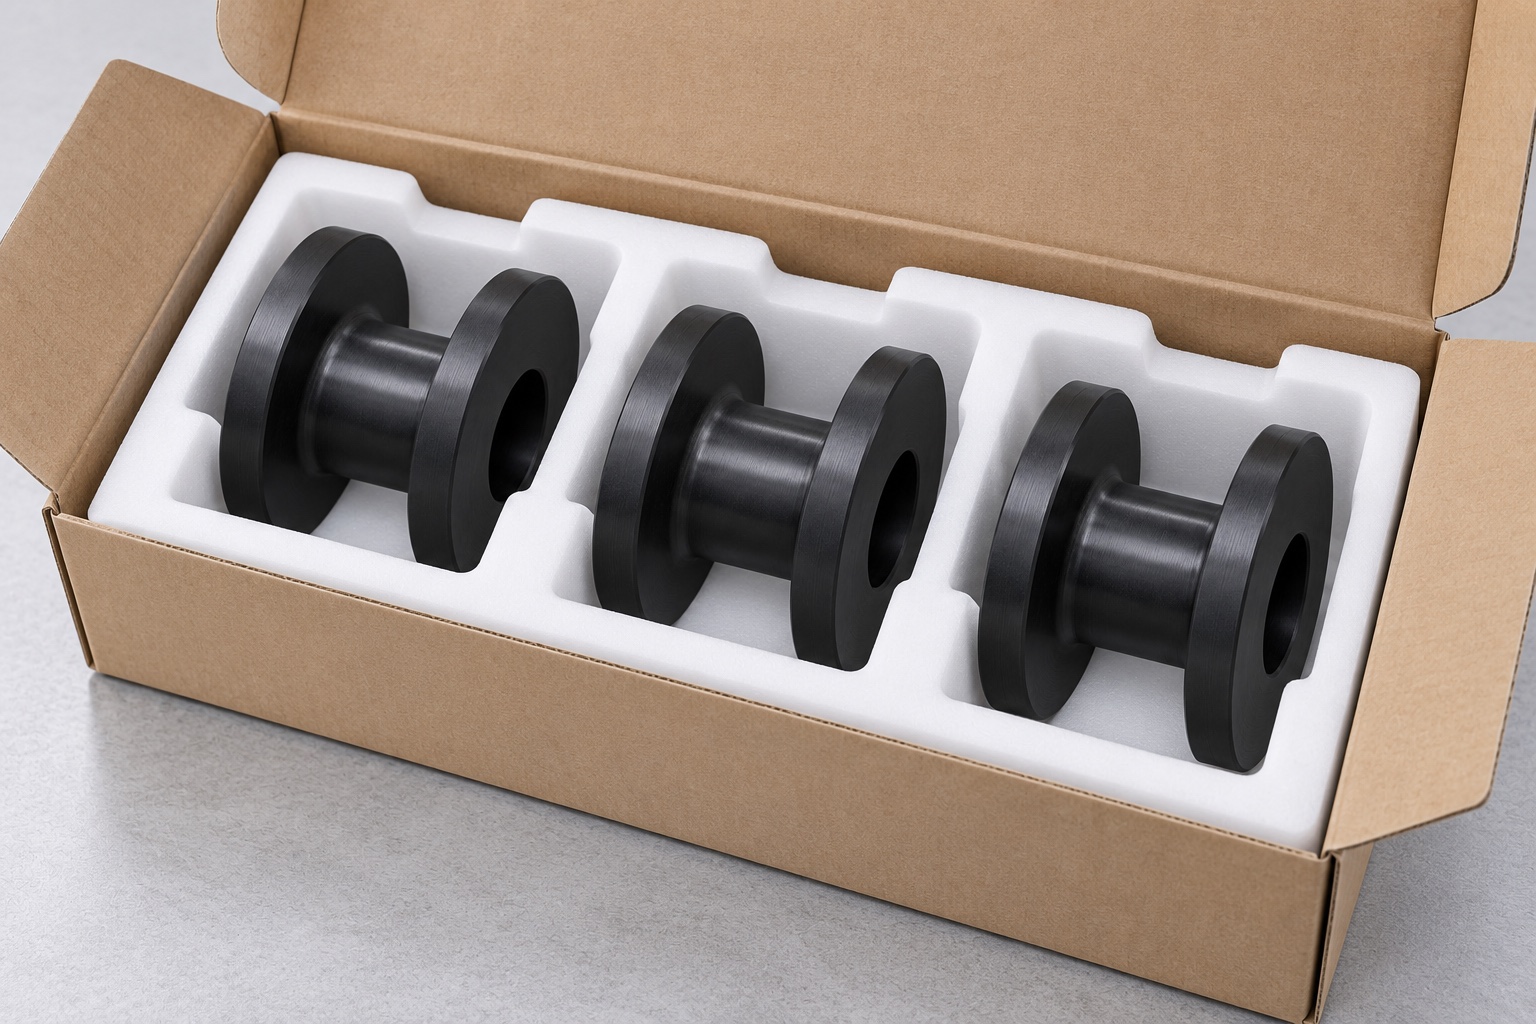
Finished spools would be separated from hard hardware so the cable-contact surface, flange roots and bore entries could not be struck during transport. Packaging support would avoid squeezing the flanges or leaving unapproved material in the contact region. Mechanical protection would not imply sterile delivery. Grade, lot, revision, conditioning and inspection status would accompany the shipment. Receiving checks would distinguish waist, bore and spacing variants, prototypes and released parts before installation. The equipment team would retain responsibility for separate routing, electrical, abrasion, maintenance and cleaning evaluations of the actual medical instrument arrangement.
Retain a route-specific repeat-order baseline
The final package would preserve released geometry, exact cable and connector, bend-radius definition, contact limits, mounting hardware, polymer evidence, final condition, inspection methods and packing scope. Approved prototype changes would become revised documents before repeat manufacture. Changes in jacket, connector, route, support or service exposure would trigger review. This representative workflow illustrates a traceable CNC turning project without inventing customer history, cable test results or finished-part medical approval, and without confusing a conforming black POM spool with a qualified strain-relief, rotating reel or validated medical equipment cable system.
Manufacturer background reference: toolbox.igus.com.
FAQ
Is this a measured customer project?
No. It is a representative proposed manufacturing workflow with illustrative component and process images. There is no actual customer delivery, sample, measurement record or achieved cable performance result. A real project would need its own released design, production records and acceptance evidence.
Does this example include a bearing or rotation?
No. Its scope is a stationary cable-contact guide with a plain bore. A rotating support, dynamic cable function or strain-relief arrangement would need its own approved geometry and evaluation instead of being inferred from the spool's appearance.
Who defines the applicable cable bend requirement?
The responsible equipment team would identify the exact cable manufacturer's requirement and its reference conditions. The machining supplier would follow the approved resulting component geometry, not invent a universal radius from cable diameter or transfer another cable's qualification.
Would connector passage justify trimming a flange?
Not without an authorized design decision. The actual cable, connector, spool and mounting configuration would be identified, and any geometry change would enter controlled documents. A hand-modified trial part would not become an informal reference for later production.
Are cable-life or electrical results claimed?
No. None are available for this representative example. Abrasion, conductor integrity, signal quality, insulation or strain relief would require separate evaluation of the complete actual route and conditions. Dimensional conformity and a static fit observation do not establish those properties.
What should repeat orders preserve?
Preserve the released spool geometry, exact cable and connector, radius definition, mounting, contact boundaries, POM grade, final condition, inspection and packing scope. Authorized changes should enter controlled revisions rather than rely on a trimmed prototype or another route's performance assumptions.
tanghangyun@oemach.com